Hygienic Design
Engineered for maximum cleanability and safety. Full CIP/SIP compatibility with Ra ≤ 0.8 µm internal finish.
Engineered for Purity
Solutions that move what matters most.
Technical Specifications
Why Fluidite
Engineered for maximum cleanability and safety. Full CIP/SIP compatibility with Ra ≤ 0.8 µm internal finish.
Gentle handling for shear-sensitive products. Low rotational speeds and large fluid pockets protect fragile emulsions, live cultures, and fruit pieces.
Built for continuous and long-lasting operation. External timing gears ensure lobes never contact each other or the casing.
Can self-prime up to 6 metres. Ideal for completely emptying tanks and hoppers without a foot valve or flooded suction.
Flow rate is directly proportional to pump speed. Adding a VFD provides precise, repeatable metering control — ideal for dosing and filling lines.
How It Works
Fluid enters the pump as the lobes create a vacuum.
Fluid is gently trapped between the lobes and the casing.
Lobes rotate, carrying the fluid towards the outlet.
Fluid is discharged smoothly with minimal shear.
Engineering
Four principles behind every Fluidite lobe pump.
External timing gears in the sealed gearbox keep both lobes perfectly synchronized. The lobes never contact each other or the casing, eliminating mechanical wear on the product stream and providing long, maintenance-free service life.
Reliable PerformanceLow rotational speeds and large fluid pockets mean the product is displaced gently. Fragile emulsions, live cultures, fruit pieces, and shear-sensitive bioproducts are transferred without damage or loss of product integrity.
Gentle on ProductsBecause every revolution displaces a fixed volume, flow rate is directly proportional to pump speed. Fitting a variable-frequency drive (VFD) provides precise, repeatable metering control — ideal for dosing and filling lines.
Precise MeteringThe expanding cavity at the inlet creates a vacuum that draws product in without a foot valve or flooded suction. Fluidite pumps can self-prime up to 6 metres, ideal for emptying tanks and hoppers completely.
Low MaintenanceBuild Quality
Product Range
Four series engineered for different process demands.
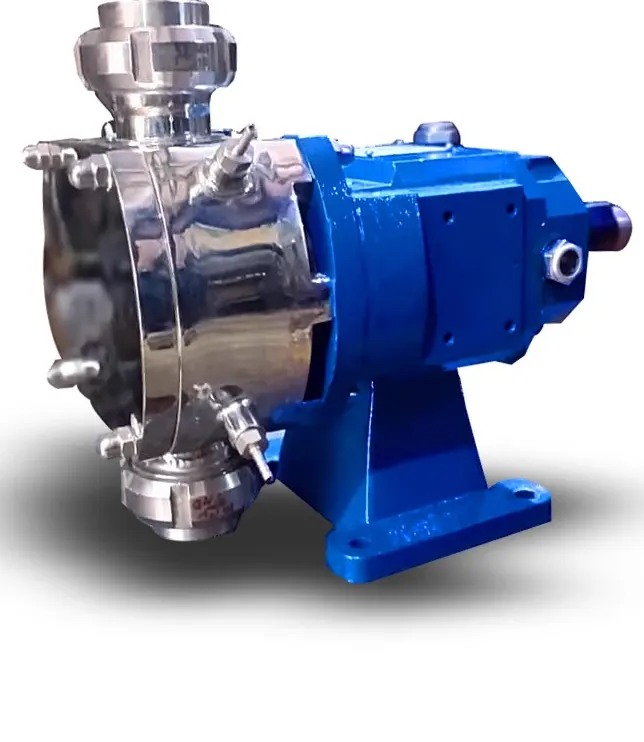
Jacketed type lobe pumps are specially designed for handling temperature-sensitive and high-viscosity products that require heating or cooling during transfer. The pump casing is provided with an external jacket (chamber) through which steam, hot water, or thermal oil circulates to maintain the desired product temperature. This prevents solidification, crystallization, or viscosity increase, ensuring smooth and continuous pumping.
Highlights
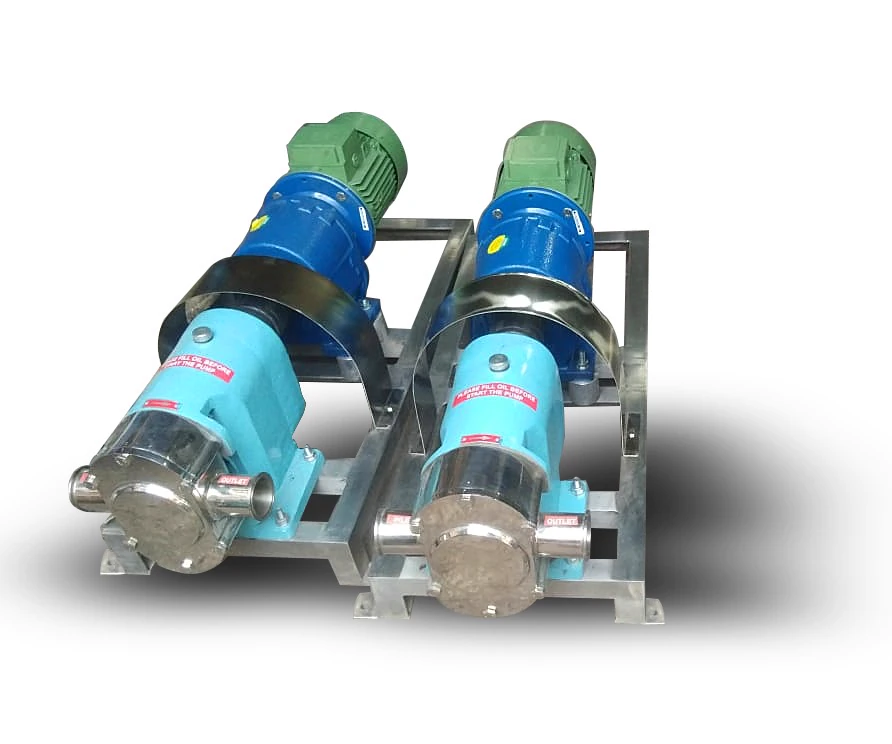
Low-profile inline configuration for space-constrained installations. Extended shaft option for direct-drive or belt-drive coupling. Stainless pump head with threaded outlet connections. Heavy-duty lobe pump with tri-clamp inlet/outlet connections. Designed for cream, butter, pastes, and thick sauces. Blue-coated gearbox with polished SS 316L pump head. Ideal for products up to 1,000,000 cP.
Highlights
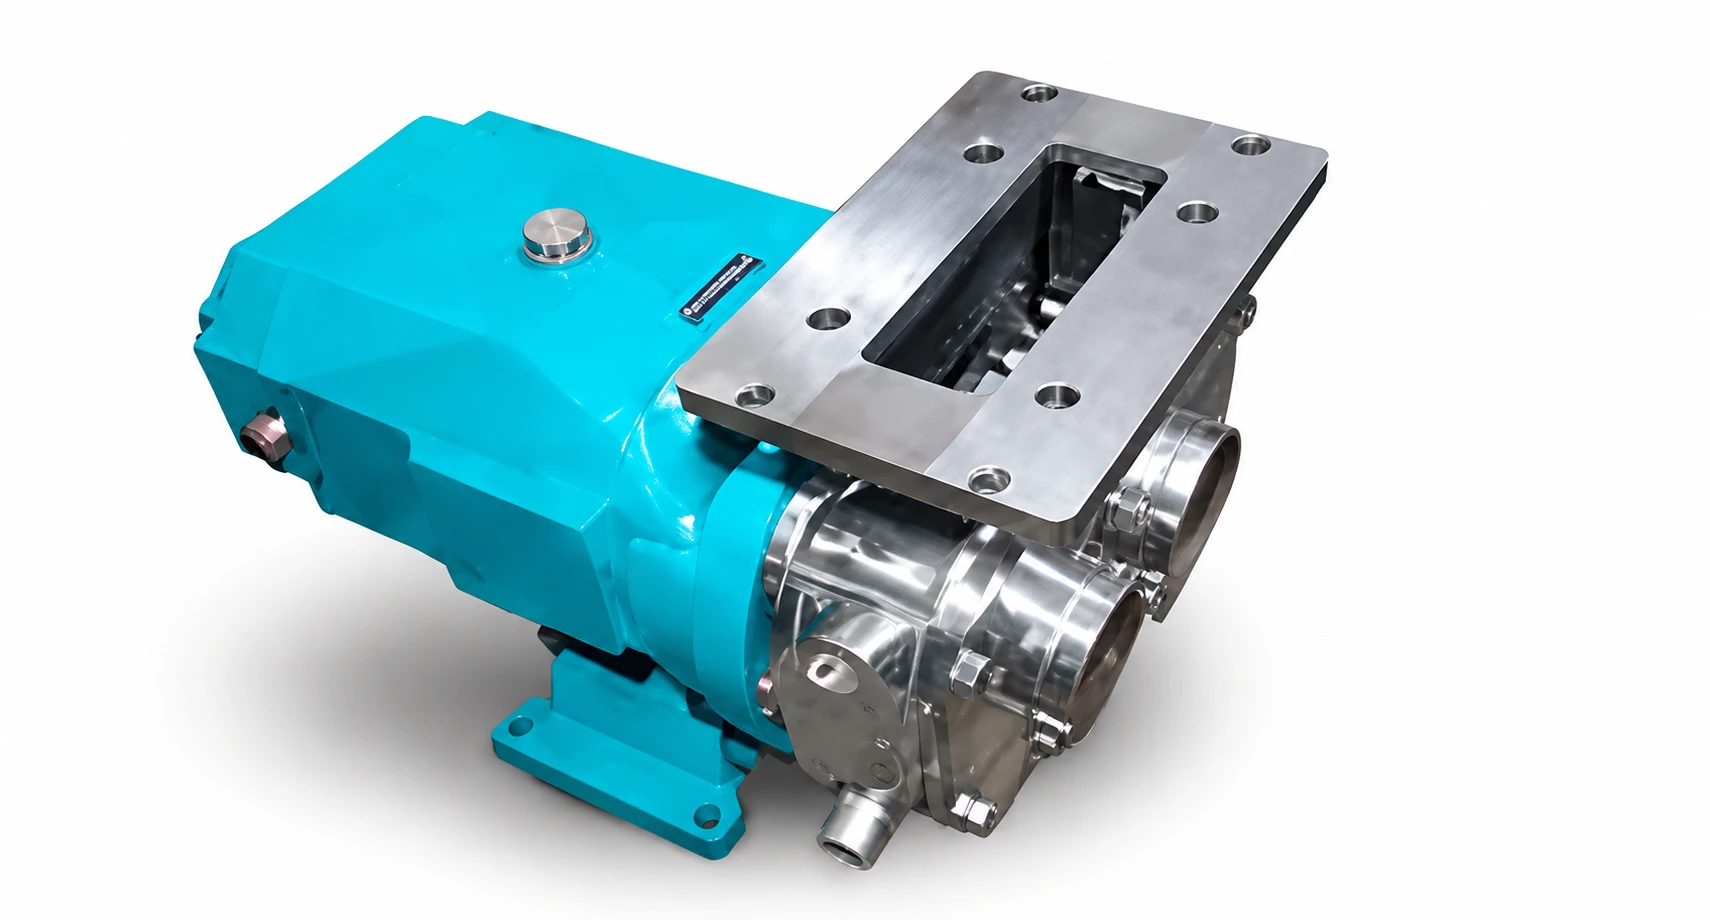
This specific configuration is designed to handle highly viscous, semi-solid, sticky, or chunky products that cannot easily flow through standard circular pipes or tend to bridge and block a conventional inlet.
Highlights
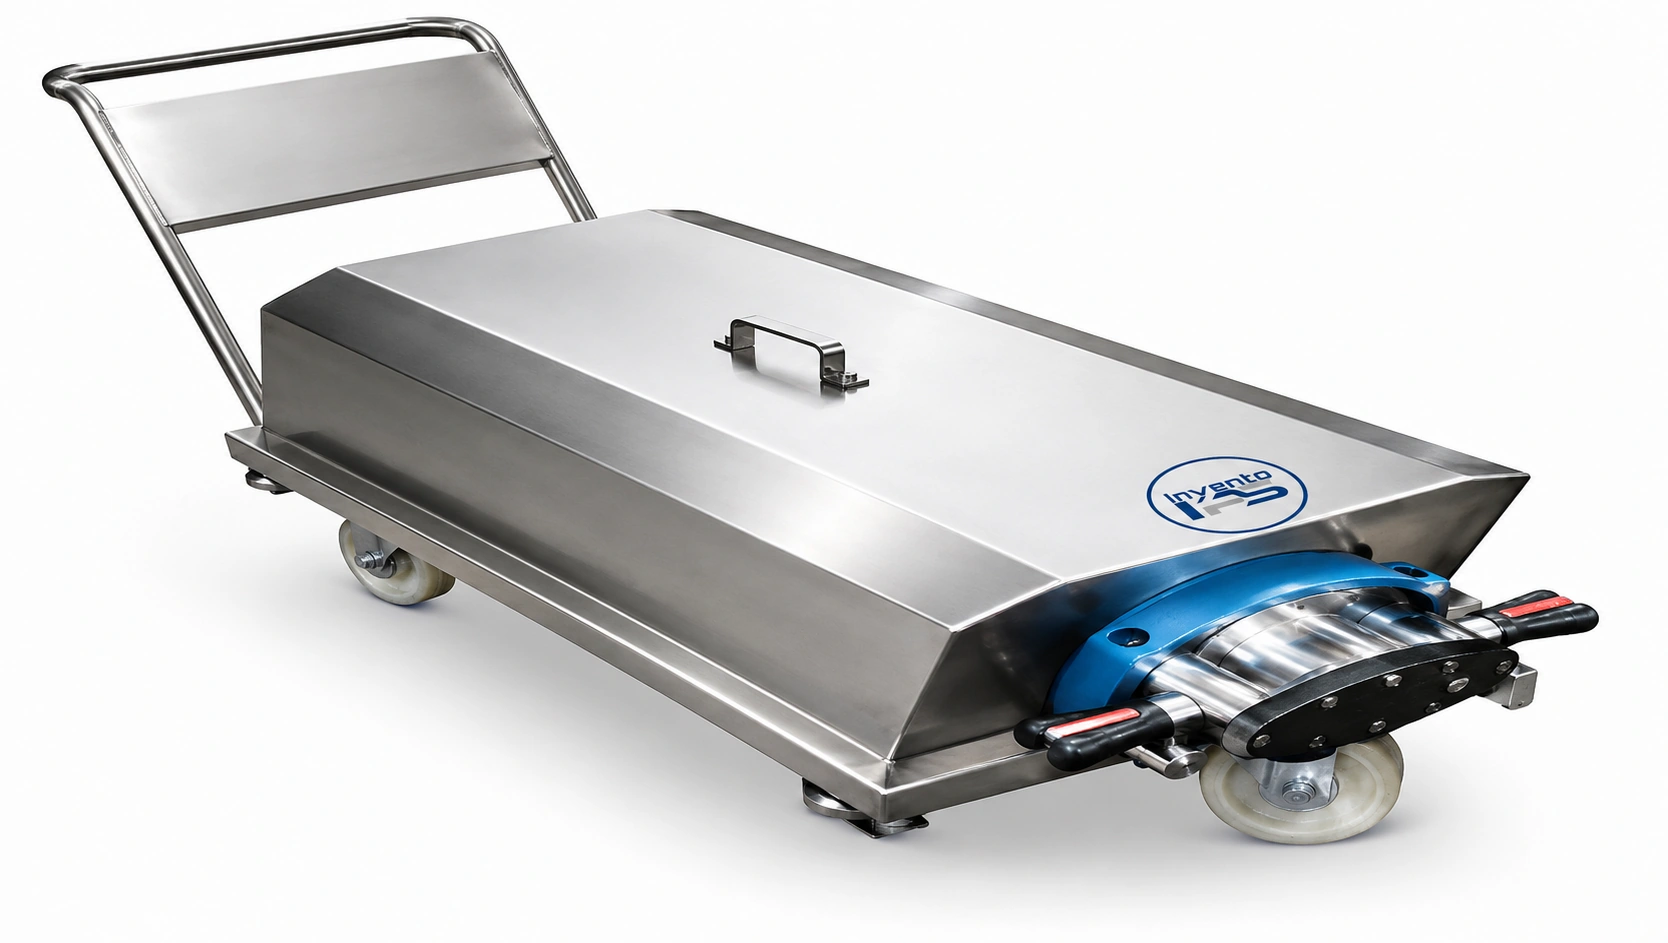
Trolley-mounted (or mobile) rotary lobe pumps are used wherever process fluids need to be transferred across multiple locations within a facility, or when a temporary, flexible pumping solution is required. Instead of being bolted down in a fixed pipework system, the pump, motor, and gearbox drive are integrated into a compact, wheeled stainless steel or heavy-duty steel cart (trolley).
Highlights
Applications
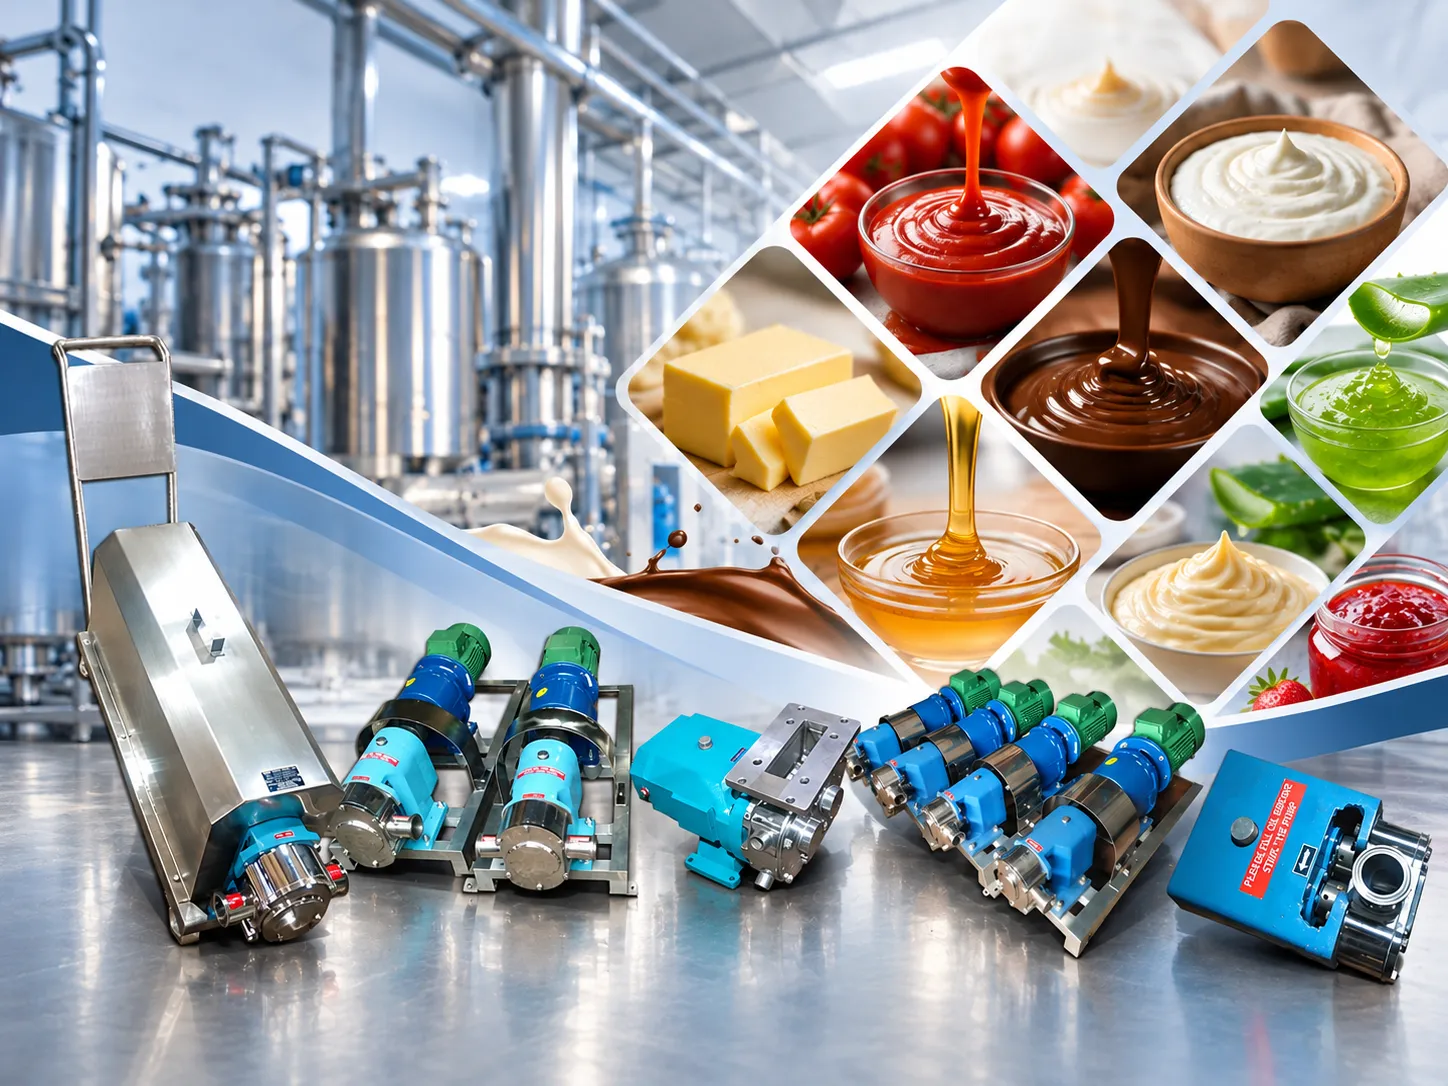
Viscous & hygienic fluids across food, dairy, and pharmaceutical industries.
Gentle handling preserves the emulsion structure essential to whipping performance.
High-viscosity tomato products with fruit and seed particulates are conveyed smoothly without separating solids from the liquid base.
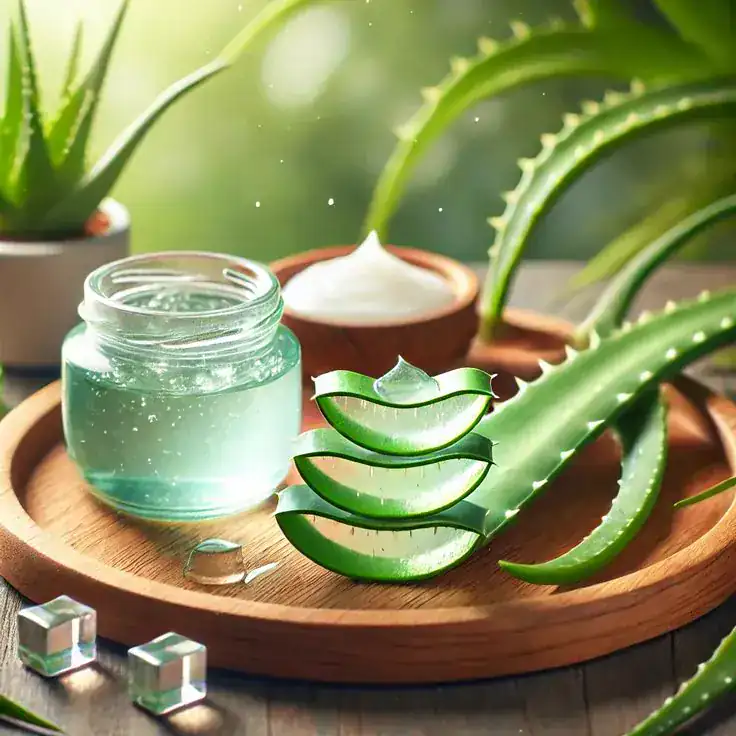
Fragile aloe gel matrix is transferred completely intact — no degradation of active polysaccharides or aloin constituents — for cosmetic, personal care, and nutraceutical applications.
Semi-solid fats at temperatures between 40°C and 80°C are pumped without smearing, churning, or heat build-up.
Delicate curd structure is maintained through slow lobe speed and gentle displacement.
Dense, high-fat pastes with abrasive solid particles demand special attention.
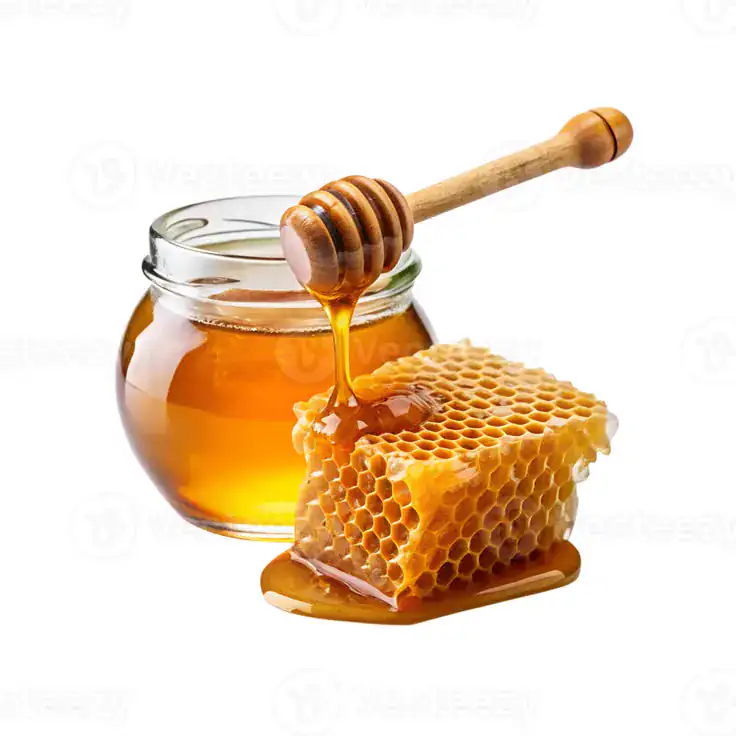
High-sugar, high-viscosity syrups up to 1,000,000 cP are handled smoothly.
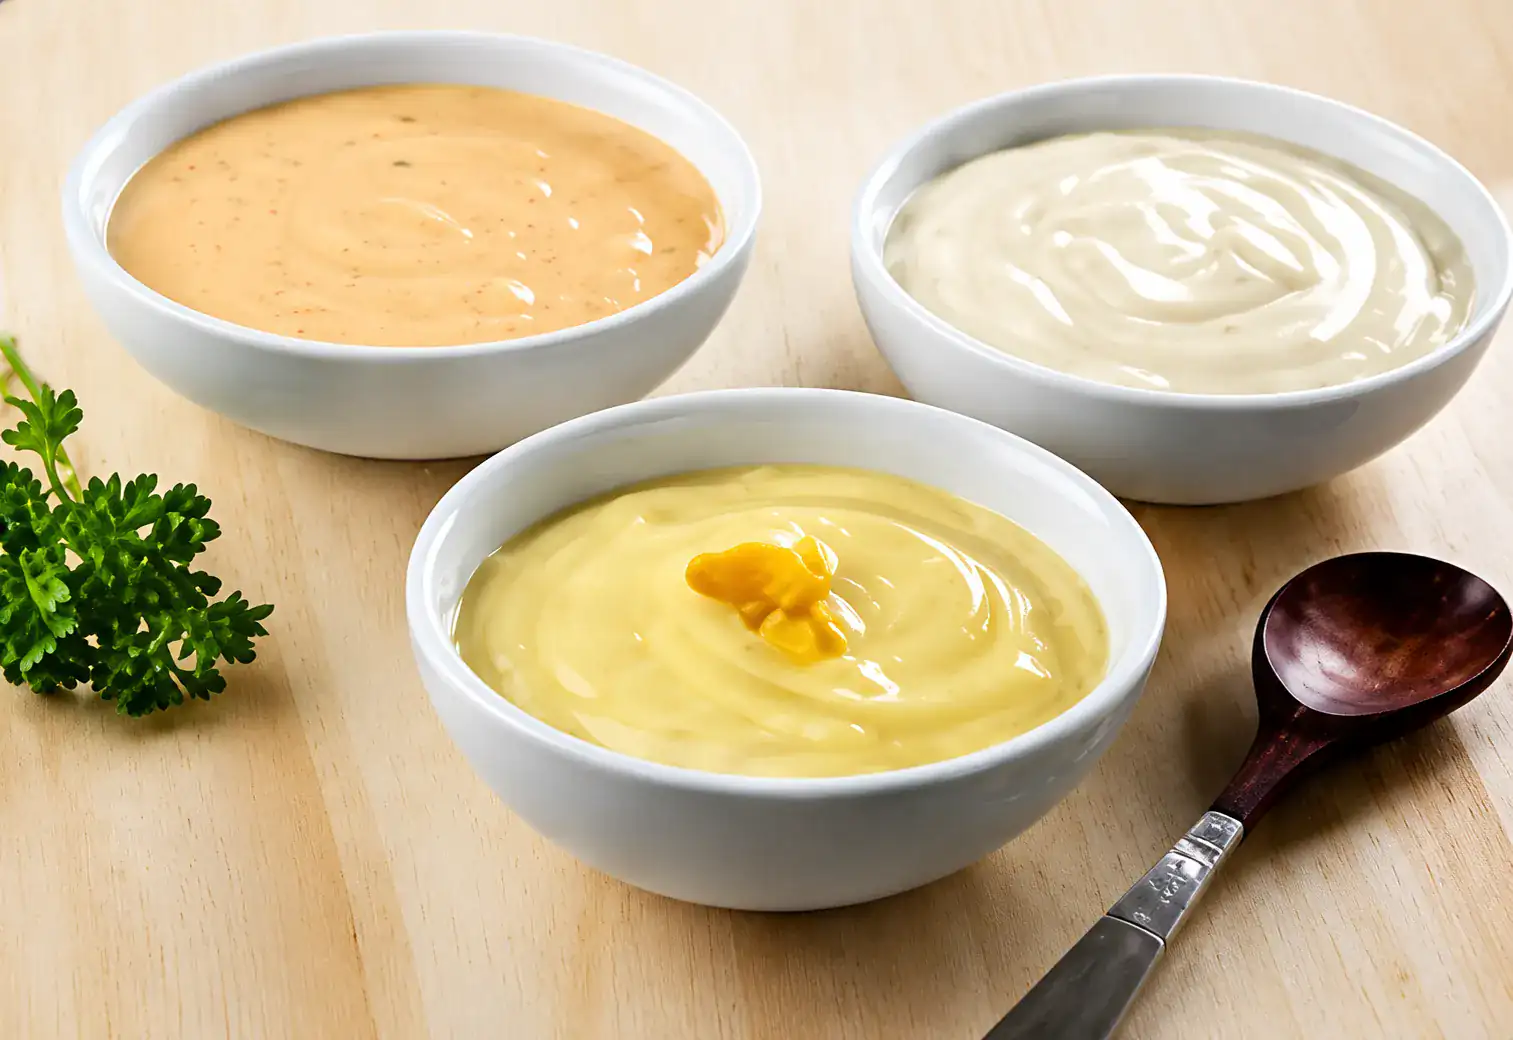
Oil-in-water emulsions are transferred without breaking the emulsion or causing phase separation.
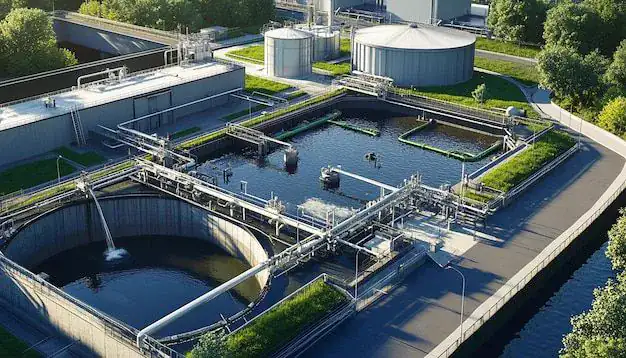
Non-hygienic cast-iron variants of the Fluidite range handle biological sludge, filter cake feed, and thickened effluent in municipal and industrial water treatment plant applications.
Industries Served
Transfer of raw milk, cream, condensed milk, cheese curd, whey concentrate, yoghurt, and flavoured dairy products across pasteurisation, homogenisation, and filling stages. Full compliance with 3-A sanitary standards.
Sauces, pastes, jams, fruit concentrates, edible oils, coconut milk, soups, and ready-to-eat foods. Gentle lobe action preserves texture and particle integrity throughout the production process.
Sterile transfer of ointments, gels, syrups, emulsions, nutritional supplements, and active pharmaceutical ingredients. GMP-compliant design with full documentation and material traceability.
Body lotions, shampoos, shower gels, face creams, aloe vera-based products, and hair conditioners. Stainless wetted parts resist aggressive formulations; easy strip-down for rapid product changeover.
Adhesives, resins, polymer solutions, wax, paint, printing inks, and polymer dispersions. High differential pressure capability and hardened rotor options extend service life in abrasive media.
Biological sludge transfer, thickened effluent pumping, filter cake feed, and chemical dosing in municipal and industrial water treatment plants. Heavy-duty cast-iron variants for continuous-duty sludge service.
Groundnut paste, peanut butter, chocolate mass, cocoa butter, vegetable shortening, and edible fats. Temperature-jacketed options for products that solidify at ambient conditions.
Our engineering team will help you select the right series, seal configuration, and drive option for your process.
+91 7798902383 · sales@inventoprocess.com
Engineered for Purity
Solutions that move what matters most.
Technical Specifications
Why Fluidite
Engineered for maximum cleanability and safety. Full CIP/SIP compatibility with Ra ≤ 0.8 µm internal finish.
Gentle handling for shear-sensitive products. Low rotational speeds and large fluid pockets protect fragile emulsions, live cultures, and fruit pieces.
Built for continuous and long-lasting operation. External timing gears ensure lobes never contact each other or the casing.
Can self-prime up to 6 metres. Ideal for completely emptying tanks and hoppers without a foot valve or flooded suction.
Flow rate is directly proportional to pump speed. Adding a VFD provides precise, repeatable metering control — ideal for dosing and filling lines.
How It Works
Fluid enters the pump as the lobes create a vacuum.
Fluid is gently trapped between the lobes and the casing.
Lobes rotate, carrying the fluid towards the outlet.
Fluid is discharged smoothly with minimal shear.
Engineering
Four principles behind every Fluidite lobe pump.
External timing gears in the sealed gearbox keep both lobes perfectly synchronized. The lobes never contact each other or the casing, eliminating mechanical wear on the product stream and providing long, maintenance-free service life.
Reliable PerformanceLow rotational speeds and large fluid pockets mean the product is displaced gently. Fragile emulsions, live cultures, fruit pieces, and shear-sensitive bioproducts are transferred without damage or loss of product integrity.
Gentle on ProductsBecause every revolution displaces a fixed volume, flow rate is directly proportional to pump speed. Fitting a variable-frequency drive (VFD) provides precise, repeatable metering control — ideal for dosing and filling lines.
Precise MeteringThe expanding cavity at the inlet creates a vacuum that draws product in without a foot valve or flooded suction. Fluidite pumps can self-prime up to 6 metres, ideal for emptying tanks and hoppers completely.
Low MaintenanceBuild Quality
Product Range
Four series engineered for different process demands.
Jacketed type lobe pumps are specially designed for handling temperature-sensitive and high-viscosity products that require heating or cooling during transfer. The pump casing is provided with an external jacket (chamber) through which steam, hot water, or thermal oil circulates to maintain the desired product temperature. This prevents solidification, crystallization, or viscosity increase, ensuring smooth and continuous pumping.
Highlights
Low-profile inline configuration for space-constrained installations. Extended shaft option for direct-drive or belt-drive coupling. Stainless pump head with threaded outlet connections. Heavy-duty lobe pump with tri-clamp inlet/outlet connections. Designed for cream, butter, pastes, and thick sauces. Blue-coated gearbox with polished SS 316L pump head. Ideal for products up to 1,000,000 cP.
Highlights
This specific configuration is designed to handle highly viscous, semi-solid, sticky, or chunky products that cannot easily flow through standard circular pipes or tend to bridge and block a conventional inlet.
Highlights
Trolley-mounted (or mobile) rotary lobe pumps are used wherever process fluids need to be transferred across multiple locations within a facility, or when a temporary, flexible pumping solution is required. Instead of being bolted down in a fixed pipework system, the pump, motor, and gearbox drive are integrated into a compact, wheeled stainless steel or heavy-duty steel cart (trolley).
Highlights
Applications
Viscous & hygienic fluids across food, dairy, and pharmaceutical industries.
Gentle handling preserves the emulsion structure essential to whipping performance.
High-viscosity tomato products with fruit and seed particulates are conveyed smoothly without separating solids from the liquid base.
Fragile aloe gel matrix is transferred completely intact — no degradation of active polysaccharides or aloin constituents — for cosmetic, personal care, and nutraceutical applications.
Semi-solid fats at temperatures between 40°C and 80°C are pumped without smearing, churning, or heat build-up.
Delicate curd structure is maintained through slow lobe speed and gentle displacement.
Dense, high-fat pastes with abrasive solid particles demand special attention.
High-sugar, high-viscosity syrups up to 1,000,000 cP are handled smoothly.
Oil-in-water emulsions are transferred without breaking the emulsion or causing phase separation.
Non-hygienic cast-iron variants of the Fluidite range handle biological sludge, filter cake feed, and thickened effluent in municipal and industrial water treatment plant applications.
Industries Served
Transfer of raw milk, cream, condensed milk, cheese curd, whey concentrate, yoghurt, and flavoured dairy products across pasteurisation, homogenisation, and filling stages. Full compliance with 3-A sanitary standards.
Sauces, pastes, jams, fruit concentrates, edible oils, coconut milk, soups, and ready-to-eat foods. Gentle lobe action preserves texture and particle integrity throughout the production process.
Sterile transfer of ointments, gels, syrups, emulsions, nutritional supplements, and active pharmaceutical ingredients. GMP-compliant design with full documentation and material traceability.
Body lotions, shampoos, shower gels, face creams, aloe vera-based products, and hair conditioners. Stainless wetted parts resist aggressive formulations; easy strip-down for rapid product changeover.
Adhesives, resins, polymer solutions, wax, paint, printing inks, and polymer dispersions. High differential pressure capability and hardened rotor options extend service life in abrasive media.
Biological sludge transfer, thickened effluent pumping, filter cake feed, and chemical dosing in municipal and industrial water treatment plants. Heavy-duty cast-iron variants for continuous-duty sludge service.
Groundnut paste, peanut butter, chocolate mass, cocoa butter, vegetable shortening, and edible fats. Temperature-jacketed options for products that solidify at ambient conditions.
Our engineering team will help you select the right series, seal configuration, and drive option for your process.
+91 7798902383 · sales@inventoprocess.com