Blenders and Mixers
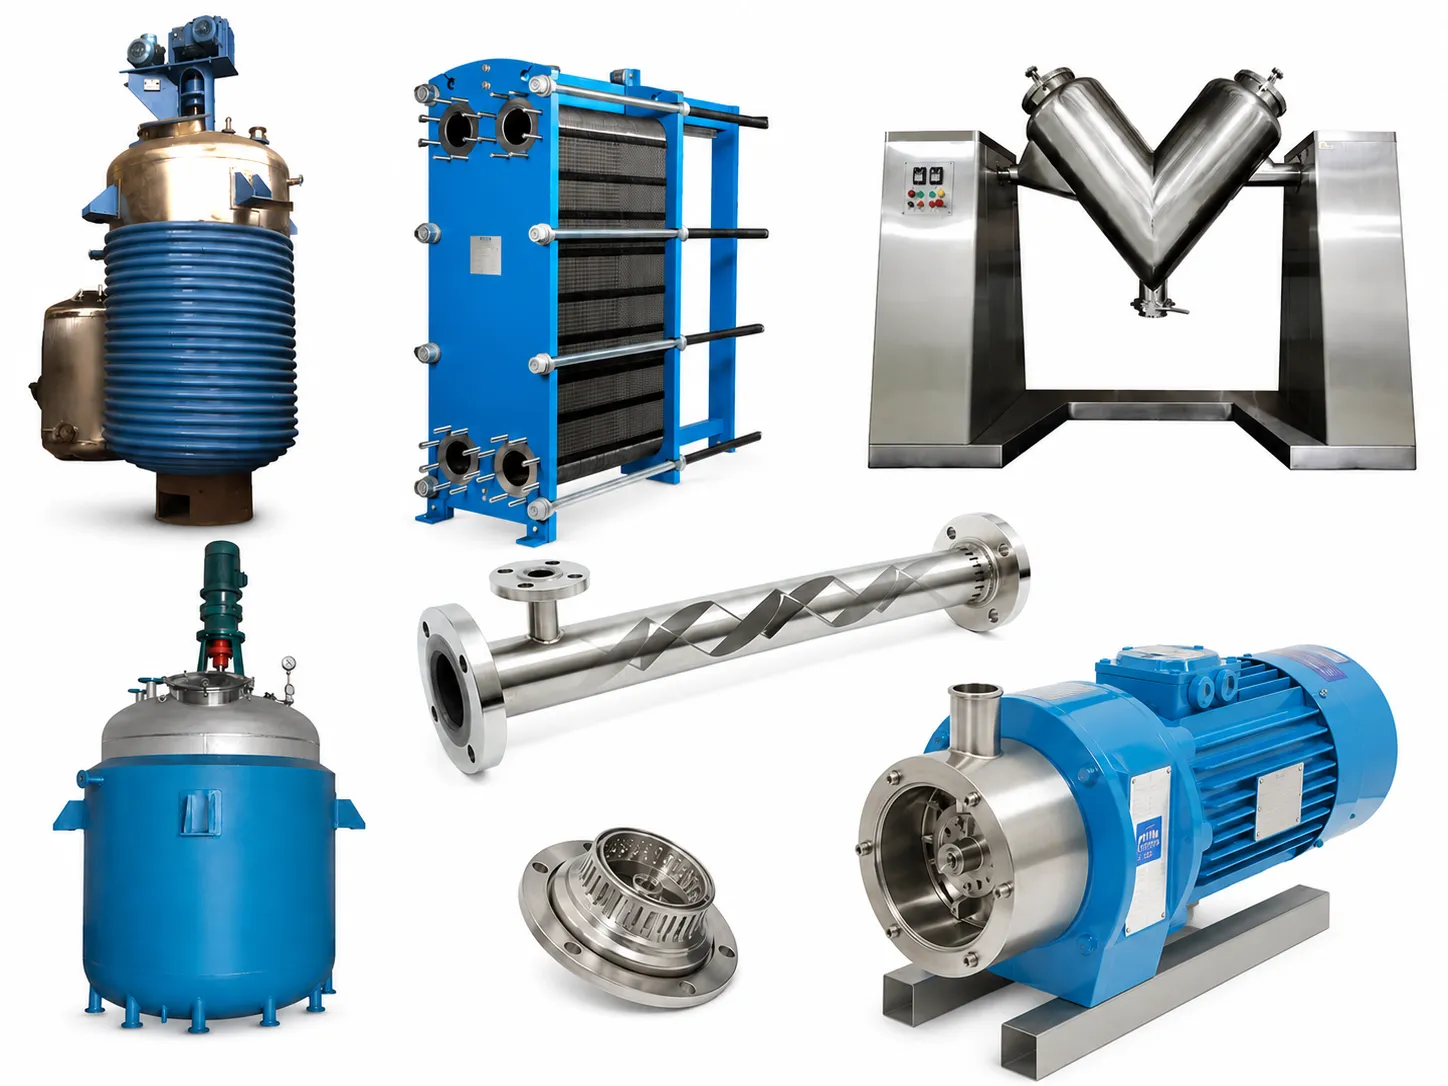
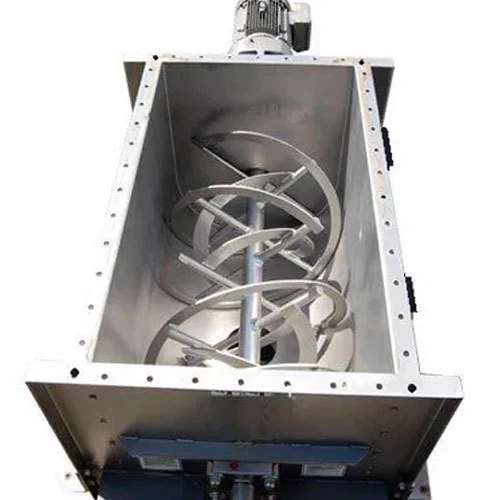
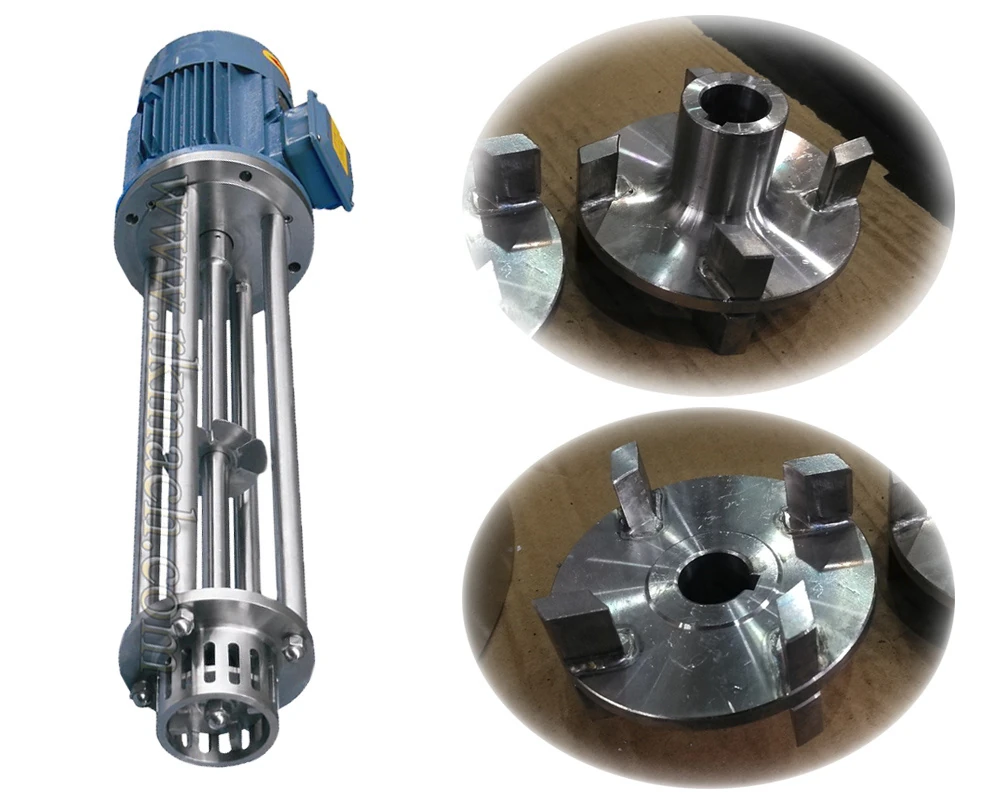
Ribbon blenders, V-blenders, double cone, octagonal, high shear, and static mixers for uniform powder and paste blending.
Key Capabilities
- Tumble & high-shear mixing
- SS304/SS316 sanitary finishes
- Capacities from 50 to 10,000 Ltrs
Engineered equipment for controlled and efficient processing.

Invento Process Solutions
Custom Engineered Systems
Manufacturing Capabilities
Manufactured in our 30,000 sq ft Pune facility with rigorous quality control, high thermal efficiency, and tailored material metallurgy for high-demand processing plants.
Fabricated with investment-grade stainless steel (SS304, SS316, SS316L), titanium, and Hastelloy. Mirror finishes down to Ra ≤ 0.8 µm ensure complete hygienic safety and cGMP compliance.
Designed for operating temperatures from -25°C to 250°C and pressures up to 12 bar (and high-pressure vessels up to 250 kg/cm²g). Single/double limpet coils and jackets maximize heat transfer efficiency.
From standalone reaction vessels and blenders to turnkey skid-mounted filtration and clean-in-place installations integrated with PLC, SCADA, and PID automated control panels.
Product Range
Browse our comprehensive range of industrial process equipment, each engineered for specialized industrial operations.

Ribbon blenders, V-blenders, double cone, octagonal, high shear, and static mixers for uniform powder and paste blending.
Key Capabilities

Plate type and shell & tube heat exchangers engineered for efficient thermal transfer in hygienic and aggressive chemical processes.
Key Capabilities

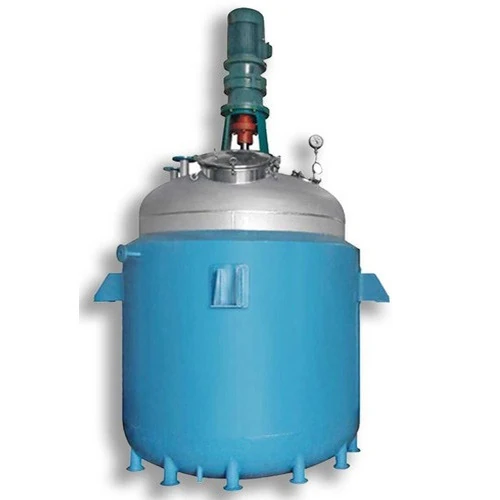
Jacketed reactors, limpet coil reaction vessels, pressure vessels, and industrial autoclaves for synthesis and pressure containment.
Key Capabilities

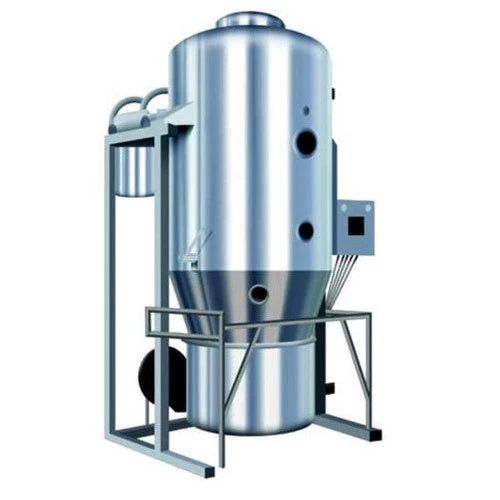
Fluidized bed dryers (FBD) and vacuum tray dryers (VTD) engineered for rapid, uniform moisture removal in pharma and chemicals.
Key Capabilities

Agitated Nutsche Filter Dryers (ANFD), candle filters, and sparkler filter presses for closed-system solid-liquid separation.
Key Capabilities

Precision-engineered agitator impellers including top entry, side entry, hydrofoil, spiral helix, Rushton turbine, and marine propellers.
Key Capabilities

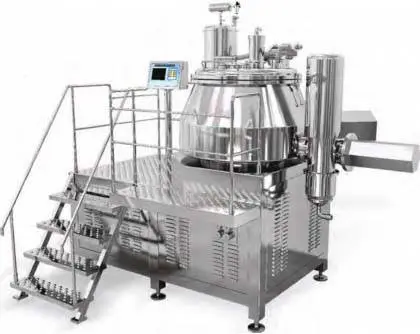
Rapid mixer granulators (RMG), multi mills, paste kettles, bead mills, colloidal mills, and vibro sifters for uniform particle sizing.
Key Capabilities

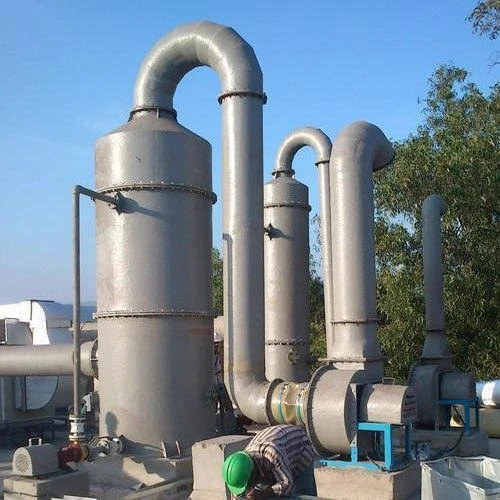
Wet and dry gas scrubber installations for intensive contact with neutralizing fluids to remove pollutant gases and recover heat.
Key Capabilities
Industry Applications
Our process equipment is installed and operating across pharmaceutical, chemical, dairy, food, and heavy industrial facilities.

cGMP reactors, ANFD filter dryers, sterile blenders, and validated CIP systems designed for zero cross-contamination.

Corrosion-resistant reaction vessels, shell & tube heat exchangers, and gas scrubbers built to withstand aggressive media.

Sanitary ribbon blenders, paste kettles, plate pasteurizers, and CIP sets conforming to 3-A sanitary guidelines.

High-pressure containment vessels, separators, and heavy-duty heat exchangers built to strict ASME standards.
Whether you need a custom-jacketed reactor, multi-stage heat exchanger, or complete automated clean-in-place system, our Pune engineering team is ready to design to your exact specifications.