Chemical & Petrochemical
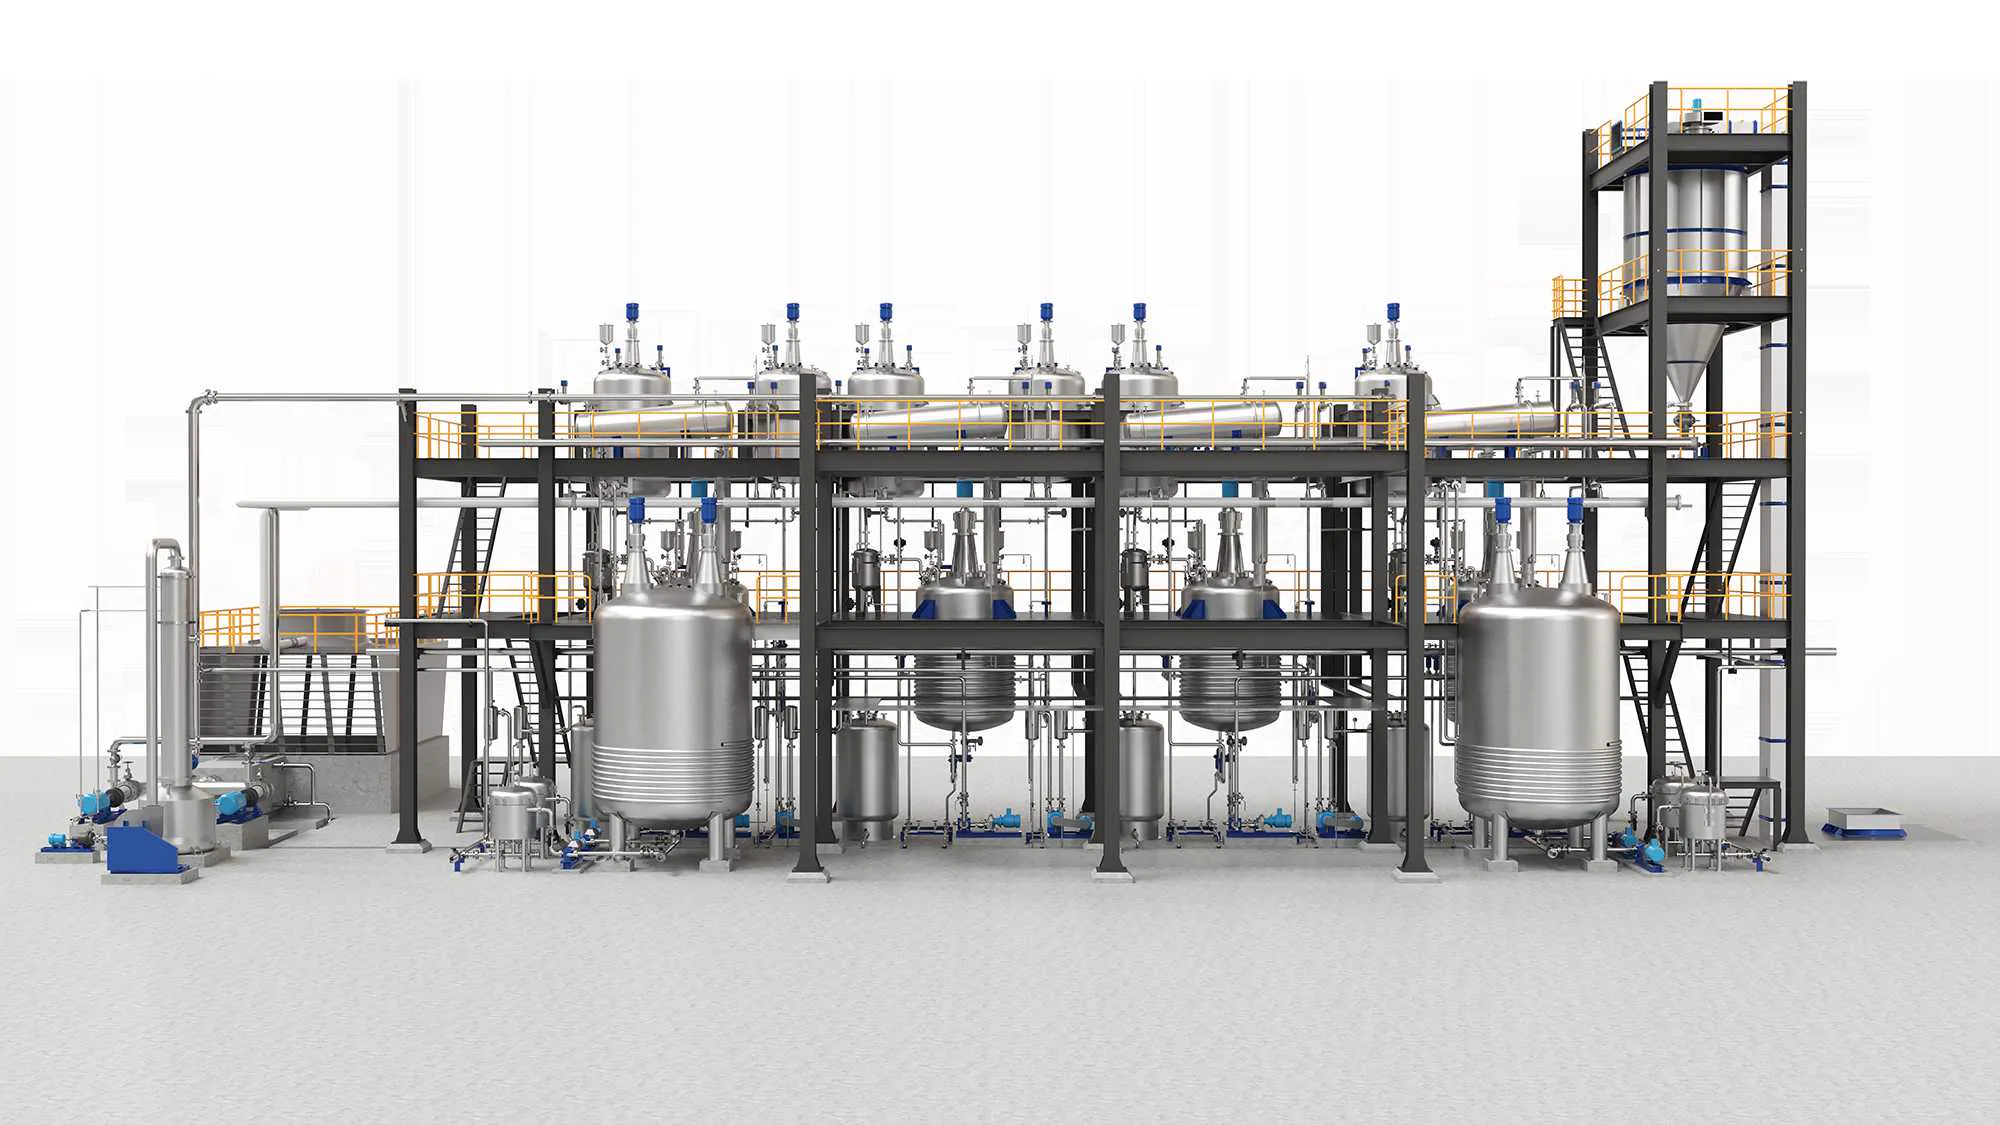
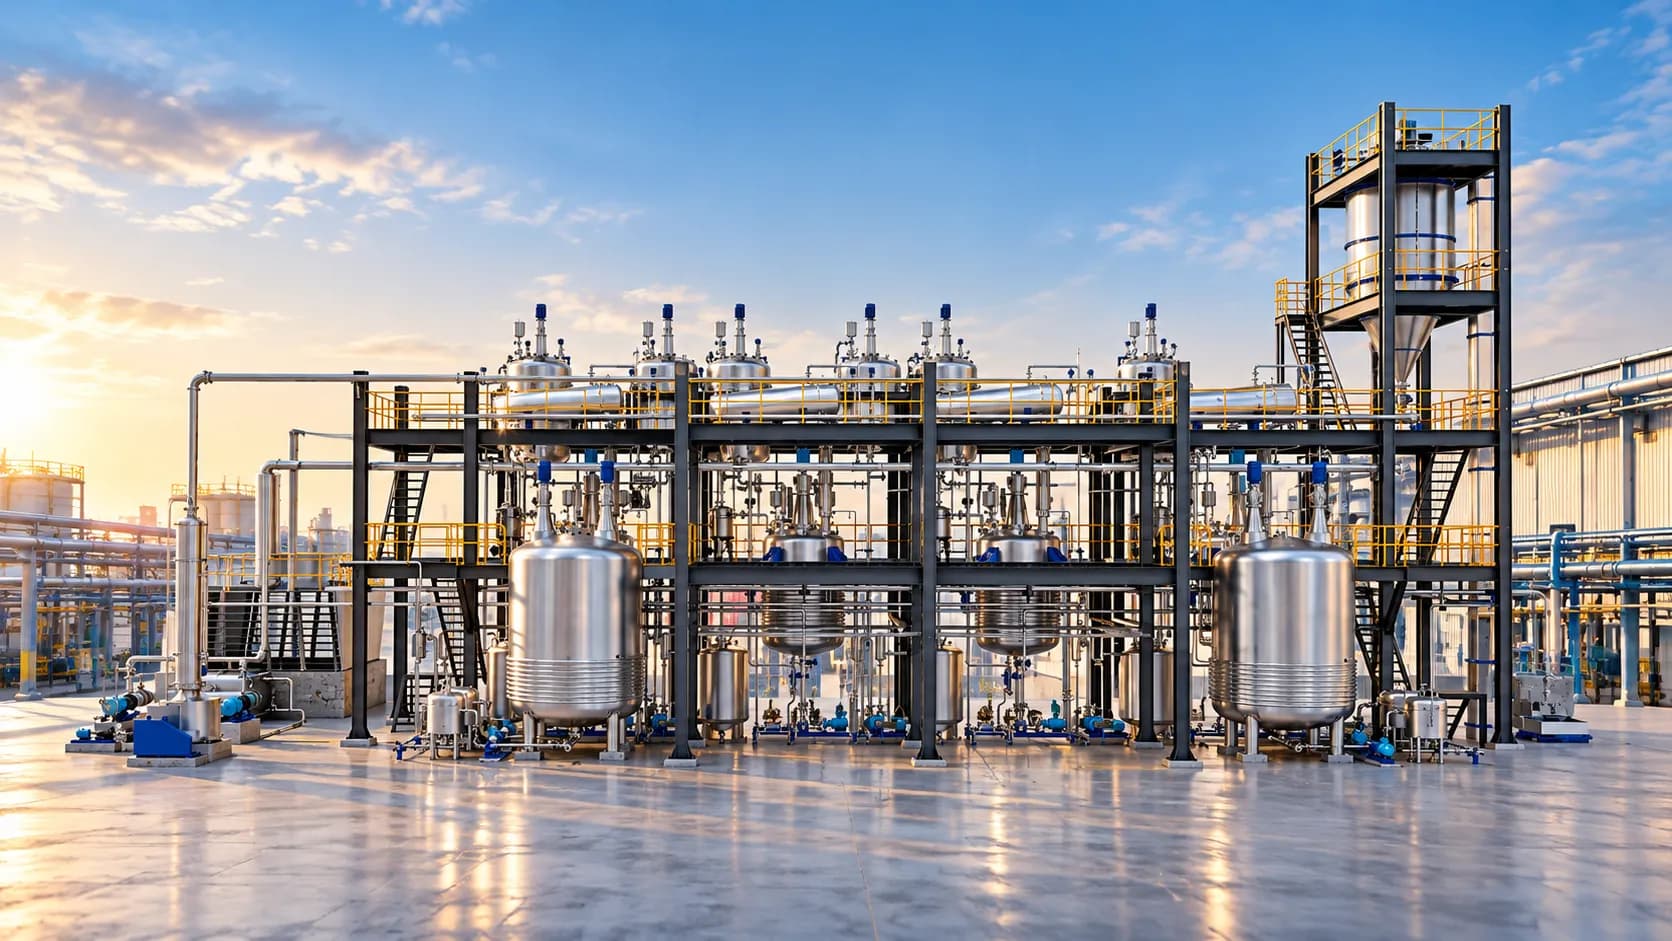
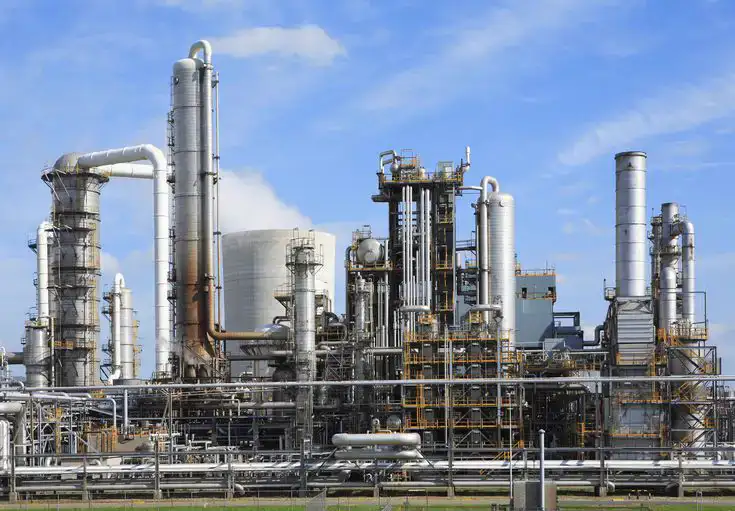
Corrosion-resistant reactors, heat exchangers, and heavy-duty pumping solutions engineered for hazardous, aggressive, and high-temperature chemical synthesis.

From fluid handling and process equipment to turnkey plants and industrial automation, we deliver solutions tailored to demanding industrial applications.
Industries We Serve
Every industry has unique operating conditions and engineering challenges. Explore the applications and solutions relevant to your business.

Corrosion-resistant reactors, heat exchangers, and heavy-duty pumping solutions engineered for hazardous, aggressive, and high-temperature chemical synthesis.

Robust fluid handling packages, high-pressure process equipment, and automated skid solutions built for demanding upstream and downstream refinery environments.

GMP-compliant sanitary granulation, milling, reaction vessels, agitated nutsche filter dryers (ANFD), and validated CIP systems for sterile formulation facilities.

Hygienic Fluidite™ rotary lobe and centrifugal pumps, paste kettles, and mixing skids for viscous, shear-sensitive dairy, beverage, and edible food products.

Sparkler filters, candle filtration units, chemical dosing skids, scrubber systems, and effluent treatment equipment for industrial zero-liquid discharge.

Turnkey ethanol distillation plants, molecular sieve dehydration units, and fermentation process skids designed for optimal yield and thermal efficiency.

Custom distillation columns, vacuum condensation skids, and acid dilution plants engineered to recycle volatile industrial solvents and reduce waste streams.

PLC control panels, MCC power distribution centers, SCADA supervisory platforms, and telemetry architectures for integrated industrial manufacturing plants.
Comprehensive Capabilities
Explore our equipment and engineering capabilities to identify solutions aligned with your process requirements.

Sanitary rotary lobe pumps, hygienic centrifugal pumps, and specialized transfer equipment engineered for gentle handling of shear-sensitive, viscous, and sanitary fluids.

Jacketed reaction vessels, limpet coil reactors, shell-and-tube/plate heat exchangers, ribbon blenders, and agitated nutsche filter dryers (ANFD) built to ASME and cGMP standards.

Custom-engineered turnkey process plants including acid dilution systems, ethanol distillation, solvent recovery plants, and liquid formulation skids with complete process integration.

Custom PLC control panels, MCC power distribution centers, SCADA supervisory platforms, and digital monitoring solutions for precise operational control and data visibility.
Our Engineering Methodology
A structured, four-phase engineering approach ensuring equipment, piping, and controls operate seamlessly under real factory conditions.
Understand the application, process requirements, fluid properties, operating conditions, and project objectives.
Evaluate suitable equipment and engineering requirements based on the application.
Coordinate relevant equipment, process systems, and automation requirements into a cohesive solution.
Explain the applicable supply, implementation, commissioning, and support arrangements based on the services InventoProcess actually provides.
Proven Applications
Real-world process engineering scenarios demonstrating equipment selection, mechanical integrity, and reliable fluid handling.
Transferring high-viscosity ointment bases and cosmetic emulsions without shearing the delicate product emulsion or introducing micro-aeration.
Fluidite™ sanitary rotary lobe pump with custom bi-wing rotor geometry, dual sanitary mechanical seals, and variable frequency drive integration.
Conducting highly exothermic, acid-catalyzed synthesis requiring strict thermal equilibrium and corrosion resistance against hot organic acids.
Custom limpet coil SS316L reaction vessel engineered with multi-pass shell-and-tube condenser and automated thermal fluid jacket control.
Elevated recurring procurement expenditure on industrial washing solvents (IPA, Acetone) and strict environmental VOC discharge restrictions.
Modular skid-mounted fractional distillation column with vacuum receiver system, plate condensers, and automated safety interlocks.
Eliminating batch-to-batch granulate density variability and reducing equipment turnaround time during product changeovers.
Rapid Mixer Granulator (RMG) integrated with automated Clean-in-Place (CIP) wash skid, dual-speed impeller drive, and validated recipe PLC controls.
The Invento Advantage
We focus on engineering compatibility, mechanical reliability, and integrated automation rather than transactional equipment sales.
Every pump, vessel, and plant component is selected around your specific rheology, temperature gradients, pressure drops, and sanitation standards rather than off-the-shelf guesswork.
We eliminate multi-vendor friction by engineering fluid transfer, heat transfer, solids mixing, and filtration as a synchronized, single-source process system.
Our comprehensive portfolio spans sanitary Fluidite™ pumps, heavy ASME process equipment, modular turnkey plants, and industrial automation under one roof.
Manufactured at our 30,000 sq ft facility in Chikhali, Pune, with rigorous stage-wise inspection, certified material test reports (MTR), and strict cGMP / 3-A conformance.
Our in-house electrical and controls team integrates custom PLC panels, MCC power gear, and SCADA telemetry directly into mechanical process skids.
Common Inquiries
Answers to common technical inquiries regarding industry applications, equipment selection, and turnkey capabilities.
Tell us about your application, process requirements, or upcoming project. Our team can help identify a suitable solution.